

Zits, blobs, and blistery “burn marks” are frustrating because they’re not one problem. On FDM printers, they’re usually a symptom of filament that’s not controlled tightly enough at the exact moment the nozzle moves.
This guide walks you through the most common causes—ooze, temperature, retraction, z-hop, dirty nozzle/liner, and cooling/bridge behavior—so you can diagnose what’s happening, then finish with a repeatable test-print checklist to stabilize results.
Understand what type of defect you’re seeing
- If bumps appear as small dots or mounds along otherwise clean walls, that points to ooze during motion (including start/stop and travel moves).
- If you see blisters, scorched spots, or dark burn marks, that often means heat is too high for the filament or the nozzle is delivering heat/flow unevenly.
- If you see blobs at layer starts, corners, seams, or where the nozzle pauses, that points toward retraction and restart behavior.
- If defects show up on bridges, overhangs, or saggy areas, it’s usually a cooling or bridge airflow mismatch.
Now work through the fixes in the order below. Even small changes can affect multiple symptoms, so each section explains what to adjust and what you should expect to improve.
Fix ooze with travel moves, wipe behavior, and flow control

What to do:
- Reduce how much time the nozzle spends “floating” without controlling flow. In the slicer, check travel behavior so travel moves are as efficient as possible (fewer unnecessary travel segments on visible surfaces).
- Enable or improve wipe (if your slicer supports it) and use a restart strategy that avoids dumping extra filament right after a pause.
- Make sure coasting/linear advance-style features (if you use them) aren’t pushing filament into the seam. These features can help, but if set too aggressively they can create a blob at the seam.
What you should see when ooze is the problem:
- The surface becomes cleaner everywhere, but you still need to tune retraction to remove “single-point” zits at motion transitions.
Reduce blisters and burn marks by dialing in temperature and heat consistency
If you’re seeing blistering, dark specks, or “burned” patches, temperature is often the culprit. Too much heat can cause excessive melt and more stringing/ooze, while poor consistency can make the first few seconds of a layer look worse than the rest.
What to do:
- Lower hotend temperature in small steps appropriate for your filament type, aiming for the lowest temperature that still produces solid layers and good interlayer adhesion.
- Watch the first layer and early layers. If they look worse (or darker) than later layers, the nozzle may be spending more time in one spot or the system may be letting heat soak too long.
- Confirm your cooling is actually working. A fan that’s misdirected, partially blocked, or failing intermittently can look like a temperature problem—especially at overhang boundaries.
What you should see when temperature is the problem:
- Fewer blistery scorches and a cleaner surface overall, plus less tendency for zits to “grow” during travel.
Tune retraction to stop blobs at starts, seams, and corners
Retraction pulls molten filament back during travel to reduce ooze. If retraction is too weak (or too slow), filament continues to leak and forms zits. If it’s too strong (or too fast), you can worsen scarring by pulling heat and creating inconsistent flow on restart.
What to do:
- Adjust retraction distance gradually. A common symptom is that zits show up right after every direction change; that usually means more retraction is needed.
- Adjust retraction speed cautiously. Speed changes how quickly pressure drops in the nozzle; too slow can still leak, too fast can cause restart problems.
- If your slicer has a minimum extrusion temperature for retraction or similar controls, make sure they’re not causing odd behavior during cooling-heavy parts.
What you should see when retraction is the problem:
- Zits cluster near the seam/starts/stops and corners, and improve as retraction strength/restart behavior becomes balanced.
Use z-hop only if you actually need it
Z-hop lifts the nozzle during travel to avoid scraping, but it can also worsen surface artifacts. The lift changes how long the filament is paused, which can encourage oozing during the pause or create a blob right as the nozzle returns.
What to do:
- If you have zits specifically after travel moves, try reducing z-hop height or disabling z-hop to see whether the artifacts decrease.
- Turn z-hop back on only if you need it to prevent dragging on high-friction surfaces (fine features, stringy materials, or previously printed textures).
- If you use z-hop with a “retract and prime” workflow, keep an eye on restart: too much added flow after z-hop can create a small mound.
What you should see when z-hop is the problem:
- You’ll notice a correlation between travel moves (especially those with lifts) and the location of the zits.
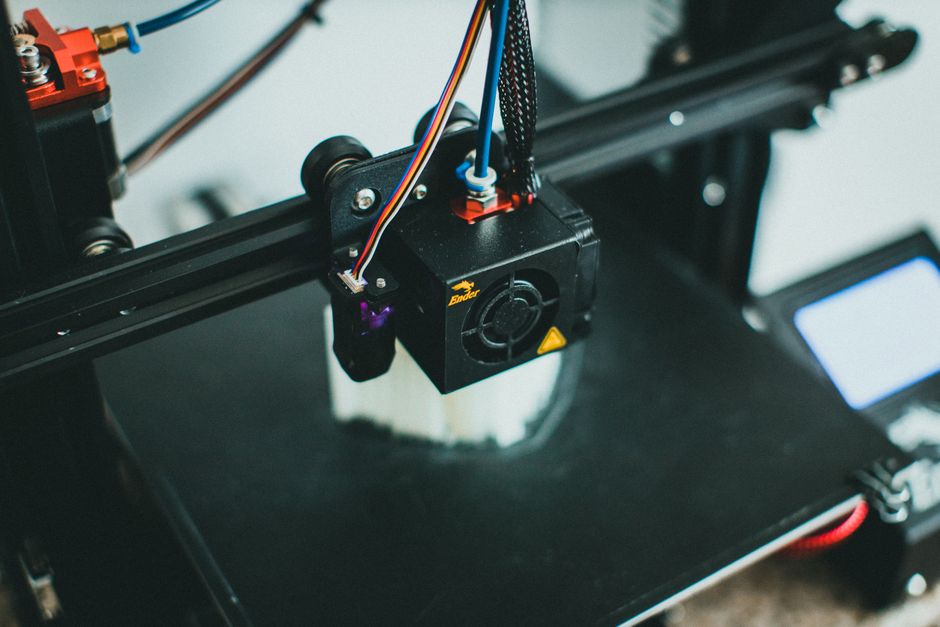
Clean and inspect the nozzle and feeding path (dirty nozzle/liner)
A dirty nozzle or inconsistent feeding path can cause intermittent flow. That’s when you get “random” zits—sometimes clustered, sometimes scattered—because the extrusion rate isn’t stable.
What to do:
- Perform a hotend cleanup using the safe cleaning method for your setup (heat to a normal printing temperature for that filament and remove residue according to your hardware guidance).
- Check for clogs or partial blockages. Even a partial restriction can cause pressure changes that look like blobs or burn marks.
- Inspect the path from extruder to nozzle. A worn or dirty liner, debris in the feed path, or inconsistent seating can create micro-pauses in extrusion.
What you should see when nozzle/liner issues are the problem:
- Artifacts vary more between prints even when you keep slicer settings identical.
Fix cooling and bridge settings to prevent scarring on overhangs
Not all “zits” are ooze. Some are surface scars from sagging material, overheated plastic, or bridges that don’t solidify quickly enough.
What to do:
- For overhangs and bridges, ensure airflow is actually reaching the part. Verify ducting, fan direction, and that nothing blocks the fan near the print.
- Match cooling strength to geometry. If the slicer uses different fan profiles for layers and features, make sure bridge settings aren’t too low (or too high) compared to the rest of the print.
- Bridge performance often depends on travel/flow timing. If bridges show blobs at the start/end points, retraction and restart tuning still matters—but so does fan behavior during those spans.
What you should see when cooling/bridge settings are the problem:
- Scarring appears mainly on overhang edges, bridging spans, or areas where the plastic needs to freeze quickly.
Run a stable test-print checklist (so the fix sticks)
Once you’ve identified the most likely cause, use a controlled test print to confirm you actually solved the root problem—without changing too many variables at once.
- Start with a known-good baseline: clean nozzle, correct filament type loaded, and a fresh, correctly seated feed path.
- Verify cooling hardware: fan direction and ducting, and confirm airflow is consistent across the print surface.
- Calibrate (or at least confirm) bed level and Z-offset so zits aren’t actually caused by excessive squish or poor adhesion.
- Reduce temperature in small steps until you reach the lowest value that still produces strong layer bonding (avoid under-extrusion that can look like defects).
- Tune retraction distance first, then retraction speed, aiming to remove seam/starts/stops blobs while keeping restart flow consistent.
- Disable z-hop temporarily (or reduce it) to see whether travel-associated zits and surface scarring improve.
- If you see issues mainly on overhangs/bridges, adjust the relevant fan profile and bridge behavior rather than changing temperature blindly.
- Enable seam and travel hygiene features (wipe/restart/coasting settings) only after retraction and temperature are stable, so you can tell which change helped.
- Print a small, repeatable test: compare the first layers, the seam areas, and one overhang/bridge feature in the same object, then change only one setting at a time for the next run.
After this checklist, your “zits and blisters” should become predictable and easier to dial in. If they don’t, treat it as a sign the problem may be hardware-related (partial clog, inconsistent feeding) rather than purely slicer settings.
PriceIt3D may earn a commission when you buy through links on this page, at no extra cost to you. Affiliate notice.