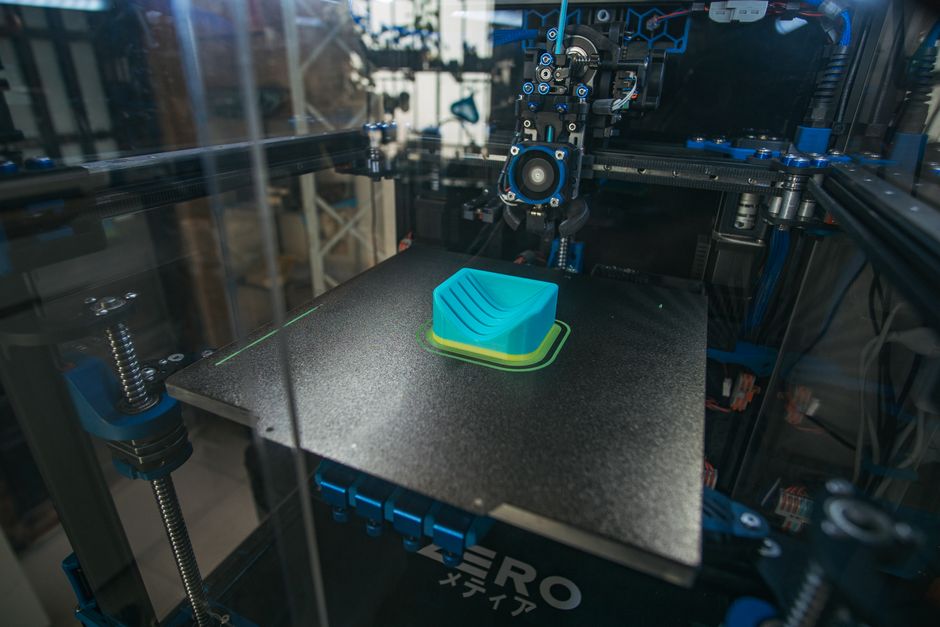

Dimensional accuracy on a resin printer isn’t “set and forget.” Lift speed, exposure time, and light smoothing all change how much resin cures during each layer, which directly affects whether holes measure right and pegs slide together.
Below, you’ll learn what each setting is doing, how to tune them in the right order, and how to verify your results with measurements you can repeat.
Why Lift Speed and Exposure Change Dimensions

- Curing defines the “shape” of the layer. Exposure time determines how much resin hardens and how far light effectively spreads beyond what you intended.
- The lift defines “mechanical stress” on the fresh layer. Lift speed (and related motion like retract/lift behavior and delays) affects whether that layer peels away smoothly or drags.
That’s why dimensional accuracy doesn’t just depend on exposure. If the printer pulls away too aggressively, small features can deform slightly—often in subtle ways you’ll notice first on small holes, thin walls, and pegs.
A practical mental model: exposure controls “how cured”, while lift speed controls “how reliably the cured layer releases.” Together, they determine whether your parts repeat.
Calibrate Lift Speed for Repeatable Geometry
Start by making sure you’re changing only lift-related settings while holding exposure constant. Then tune in this order:
- Look for release problems. If lift is too fast (or too forceful), you can get tiny artifacts, deformation near feature edges, or inconsistent hole diameters across repeats.
- Look for suction problems. If lift is too slow or includes overly aggressive dwell times, resin can continue to flow and affect the lower layers, also changing dimensional outcomes.
- Aim for “clean peel.” The best lift speed is usually the one that produces smooth, consistent surfaces on contact areas without leaving streaks or pulling marks.
What to measure on your test piece:
- Peg diameter (or width): measure at the same height for each print.
- Hole diameter: measure through the region where the hole is formed (top opening vs deeper regions can differ).
- Hole roundness: oval holes often point to release drag or inconsistent peeling.
Important: dimensional errors can repeat even when your surface looks fine. Lift calibration is about repeatability, so run at least one quick repeat once you think you’re close.
Tune Exposure Using Dimensional Test Prints
Exposure time is the other big driver. Overexposure tends to grow features (pegs get thicker; holes get smaller). Underexposure tends to do the opposite (pegs thin out; holes open up), and it can also create weak edges that degrade after post-processing.
For dimensional accuracy, don’t only rely on “did it print?”—you need targeted test geometry.
Use a test print that includes:
- Cylinders/pegs across the sizes you care about
- Through-holes or stepped holes (to see how dimension changes through depth)
- Small gaps or thin walls, if those are part of your fit design
Then tune exposure methodically:
- Change exposure in small increments, not big jumps.
- Keep lift speed fixed while adjusting exposure.
- Use the same measurement approach every time (same caliper orientation, same measurement heights).
Also remember exposure isn’t only the “main” exposure. Many slicers separate settings like bottom/initial exposure from normal layer exposure. If your holes or pegs start near the build plate, the first layers can meaningfully affect their final dimensions.
Practical takeaway: if peg diameters are consistently off but hole depths look inconsistent, you may need to tune both initial/bottom behavior and main exposure—not just one exposure value.
Control Small-Feature Accuracy With Anti-Aliasing and Light Settings
Even with perfect lift speed and exposure, small features can still measure off because slicers and printers may apply anti-aliasing / smoothing. This typically helps with stair-stepping, but it can also change how edges “blend,” which affects:
- Small-radius corners and sharp edges
- Tiny holes (where a little extra curing changes the opening size)
- Thin pegs (where edge growth changes the effective diameter)
If you notice a consistent pattern—like holes always slightly undersized or pegs always slightly fat—anti-aliasing and light smoothing settings are worth checking.
A good way to approach this is:
- Tune lift speed first so you’re not fighting mechanical release artifacts.
- Tune exposure second so you control overall cure.
- Tune anti-aliasing last so you refine edge behavior without destabilizing the baseline.
General guidance:
- If you need precision over smoothness, consider reducing anti-aliasing strength (or disabling it) temporarily during calibration.
- Once dimensional accuracy is correct, you can reintroduce smoothing carefully and re-check holes/pegs.
One more nuance: post-processing and cleaning matter for small features. If you blast holes too aggressively or allow uncured resin to linger, dimensions can change after the print finishes curing. For calibration, keep post-processing consistent so your “measured dimension” reflects printer settings, not cleaning differences.
A Repeatable Workflow to Get Holes and Pegs Measuring Right
Use this workflow to tune lift speed, exposure, and anti-aliasing without chasing noise.
- Print a calibration test geared for fit features (pegs and holes at the sizes you care about).
- Set a baseline exposure and baseline anti-aliasing (keep both fixed while adjusting lift-related settings).
- Tune lift speed for release consistency and measure peg diameter + hole roundness on at least two prints.
- Tune exposure next while keeping lift speed fixed, adjusting exposure in small steps and re-measuring the same geometry.
- Only then adjust anti-aliasing/light smoothing to correct systematic edge/roundness bias (like holes always too small or pegs always too thick).
- Lock your profile and verify repeatability by printing a final set, measuring across multiple positions/heights, and confirming the same error pattern (or none).
If results drift between runs, treat that as a sign your process variables aren’t controlled yet. The most common culprits are resin temperature, inconsistent vat leveling, variable post-curing time, or changing cleaning pressure.
Common Calibration Mistakes That Break Dimensional Accuracy
Even experienced users can get stuck because it’s easy to adjust the wrong combination of settings at once. Here are the most common causes of “it prints, but it won’t measure.”
- Changing lift and exposure simultaneously. If dimensions improve, you won’t know which setting caused it.
- Optimizing only surface look. A part can look crisp but still measure wrong if feature edges are over-cured or release is deforming them.
- Measuring the wrong height. Small holes often have slightly different diameters at the top vs deeper layers. Always measure the same zone.
- Ignoring initial/bottom layer behavior. If your parts include features close to the build plate, initial exposure and first-layer behavior can dominate accuracy.
- Letting post-processing vary. Washing time, agitation, and drying temperature can change dimensions for small holes and thin pegs.
When calibration goes off the rails, the fastest fix is to return to a controlled baseline: one change at a time, and one test print you can measure consistently.
Once your holes and pegs land where they should on a repeatable test, dimensional accuracy becomes predictable—then you can safely focus on fit, finish, and surface quality without sacrificing measurement confidence.
PriceIt3D may earn a commission when you buy through links on this page, at no extra cost to you. Affiliate notice.