

Resin that doesn’t cure cleanly can cause delamination, weak layers, tacky prints, and hazy or cloudy-looking results. The good news: most of these failures trace back to a few predictable problems in the workflow—especially exposure, resin cleanliness, and post-curing.
Below is a practical troubleshooting path you can follow step-by-step, then the specific checks to prevent the same issues from coming back.
Match the symptom to the stage
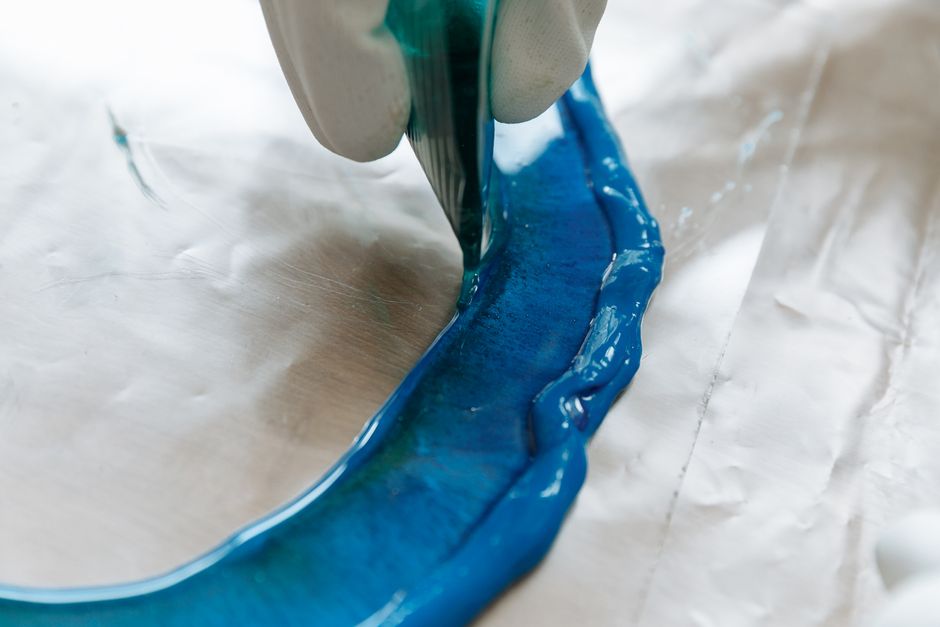
Look at your print after the pull and after washing:
- If the part looks structurally separated between layers right after printing, think exposure, Z/adhesion, and lift behavior.
- If layers look okay initially but the part stays soft, tacky, or hazy after post-curing, think wash/dry steps and curing intensity/coverage.
- If the resin in the vat is visibly cloudy or has odd particles, think contamination and filtration before you touch exposure settings.
Run the checks in order (most likely fixes first)
- Confirm the resin type matches the process (some resins are designed for different curing approaches). If you mixed brands/types, symptoms like haziness or weak bonding are common.
- Check resin temperature and storage condition. Cold resin can cure inconsistently and lead to weak layer adhesion; overly aged or repeatedly UV-exposed resin can behave unpredictably.
- Verify build plate and vat cleanliness. Fingerprints, residue, dust, or dried resin films can reduce adhesion and cause partial delamination.
- Re-check exposure using a small calibration print before reprinting the job. A quick test designed for your resin helps confirm whether layers are fully bonding.
- Adjust lift/settling behavior if delamination is layer-by-layer. Too-rapid lift, inadequate rest time, or aggressive motion can disturb uncured layers and prevent proper bonding.
- Filter and strain the resin before printing again. Cloudy vat resin or visible specks often come from contamination; filtration also catches debris that can scatter light.
- Improve washing consistency and drying. Residue from cleaning liquid can block UV during curing and make surfaces look hazy.
- Post-cure with correct time/intensity and even coverage. Use a curing enclosure if you have one, and ensure the part isn’t shaded or stacked unevenly. For example, SUNLU UV Resin Curing Box helps deliver more consistent exposure compared to leaving parts under a lamp.
- Prevent recurrence with better handling: keep lids closed, avoid UV exposure of the bottle, and don’t pour contaminated resin back into stock.
Calibrate exposure for strong layer adhesion
Delamination often happens when layers don’t bond well—either because each layer isn’t exposed long enough, or because mechanical forces during printing break the forming structure.
Begin with the factors that most directly change bonding quality:
1) Exposure calibration (bottom layers and regular layers)
If the first layers don’t bond strongly enough to the build plate, the job can detach and start failing early. If regular layers underexpose, you can get layer separation later—sometimes starting as wispy cracks, then growing into full delamination.
Fix approach:
- Use a purpose-built resin test to dial in exposure for your printer and current resin batch.
- After you update exposure, print a small, representative piece (with similar thickness and geometry) rather than jumping straight to the main model.
2) Z offset and adhesion to the build plate
Even correct exposure can fail if the plate-to-film distance isn’t right. If adhesion is too weak, the print can detach between layers; if it’s too strong, you can increase stress during the lift cycles.
Fix approach:
- Reconfirm leveling and Z/offset settings.
- Clean the build plate properly and avoid leaving streaks or residues.
3) Print motion and lift behavior
Resin printers repeatedly separate the film and part during each layer transition. If motion parameters are too aggressive or rest/settle times are too short for your resin viscosity, layers can be disturbed before they’re fully cured.
Fix approach:
- If delamination patterns match lift cycles (often consistent at similar heights), focus on lift speed and rest timing.
- Re-tune gradually—change one motion parameter at a time and re-test with a small model.
4) Geometry and thickness
Thin features can cure “faster” or appear fully formed while internal volumes remain undercured. That can show up as partial delamination during post-curing or handling.
Fix approach:
- For difficult models, test with an orientation that reduces unsupported spans and thick-to-thin transitions.
- Consider adding supports and reducing large flat surfaces that trap uncured resin.
Keep the resin clean with filtration and handling
Cloudy resin in the vat is one of the clearest signs that something is contaminating your resin or affecting how light passes through it. Even small particles can scatter light and reduce effective exposure, which then leads to both weak bonding and hazy results.
Common contamination sources include:
- Dust introduced during bottle handling or topping-off
- Dried resin flakes from funnels, funnels/strainers, or the vat walls
- Water/IPA residue from splashback or improper cleaning of tools
- Leftover resin from earlier prints poured back into the working tank
Practical prevention checks:
1) Strain and filter before every serious run
If you see floaters, cloudiness, or sediment, strain the resin using the correct filter method you trust for your workflow. Don’t assume “it looks fine” is good enough—tiny debris can be invisible until it affects cure quality.
2) Avoid mixing “old” and “new” without a plan
Reusing resin can be fine, but only if it’s clean and consistent. If a previous job failed due to exposure mismatch or you suspect contamination, treat that resin cautiously.
3) Keep surfaces uncontaminated
Clean the inside of the vat area (with the appropriate safety steps for your setup) so cured flakes don’t re-enter the resin.
4) Control where resin spends time
Resin naturally collects contaminants during repeated handling. Limit how long resin is left open, and store bottles properly when not actively in use.
When the resin is clean again, you can usually tell quickly: the next calibration print should have crisper edges and better layer cohesion, and the haziness in the vat should drop.
Post-cure correctly to avoid soft or hazy prints
Many “curing issues” aren’t actually cured failures—they’re wash, dry, and post-cure coverage problems.
1) Washing residue can block UV
If solvent or residue remains on the part, UV may not penetrate as effectively. That can produce cloudy surfaces, weak internal structure, and inconsistent curing across the part.
Fix approach:
- Wash thoroughly and consistently.
- Let parts dry so surfaces aren’t holding cleaning liquid.
- Avoid leaving prints damp in a way that delays curing.
2) Even curing requires coverage and orientation
Parts often shade each other or hide surfaces from the curing light. Supports can also create tiny pockets where resin doesn’t get the same exposure.
Fix approach:
- Cure in a way that rotates or exposes all sides.
- If your parts are complex, consider separating them rather than stacking.
3) Under-curing vs over-curing
Under-curing often shows up as tackiness, low stiffness, and hazy surfaces that don’t improve much no matter how long you “spot cure.” Over-curing can bring its own problems (brittleness and discoloration), so adjust in the direction your resin recommends rather than endlessly extending cure time.
If you’re seeing haziness after curing, increase cure consistency first (coverage, drying, orientation), then fine-tune exposure-related curing settings.
Protect the vat and final parts from cloudiness
Cloudy resin complaints come from two broad buckets: cloudy vat resin (light scattering or contamination) and cloudy final parts (wash residue, incomplete curing, or incompatible handling.
Cloudy vat resin
If the liquid in the vat looks milky, hazy, or “dirty,” treat it as a root-cause issue:
- Filter/strain it and confirm your workflow prevents new contamination.
- Check whether the resin has been exposed to UV light more than intended (for example, left in bright light). Degraded resin can cure unevenly.
- Make sure the environment isn’t introducing moisture via wet tools or improper storage.
Cloudy final parts
If the vat looks clear but the finished parts are hazy:
- Re-check your wash and drying steps—residue is a very common cause.
- Confirm post-cure consistency (including coverage and timing).
- If only certain regions are cloudy (for example, recessed areas or internal pockets), it usually indicates incomplete cure due to shading or poor penetration.
A helpful diagnostic pattern: if the part is structurally solid but looks hazy, the cure likely isn’t uniform or washing left residue. If the part also feels weak or separates between layers, focus on exposure calibration and adhesion first.
Keeping these checks aligned—exposure for bonding, filtration for clarity, and post-cure for complete curing—removes most delamination and cloudiness problems without chasing random setting changes.
PriceIt3D may earn a commission when you buy through links on this page, at no extra cost to you. Affiliate notice.