

Nylon 6 and nylon 12 are both favorites for functional 3D prints, but they don’t behave the same once your parts are in the real world. If you want durable parts that hold up over time, you’ll need to match the nylon type to moisture sensitivity, printing approach, and expected creep under load.
This guide walks through how nylon 6 vs nylon 12 differs, what that means for print quality and reliability, and which nylon type fits common functional use cases.
Nylon 6 for Tough, Practical Functional Prints
What it tends to do well
- Impact and toughness: Nylon 6 is a strong pick for parts that see shocks, vibration, and repeated flexing.
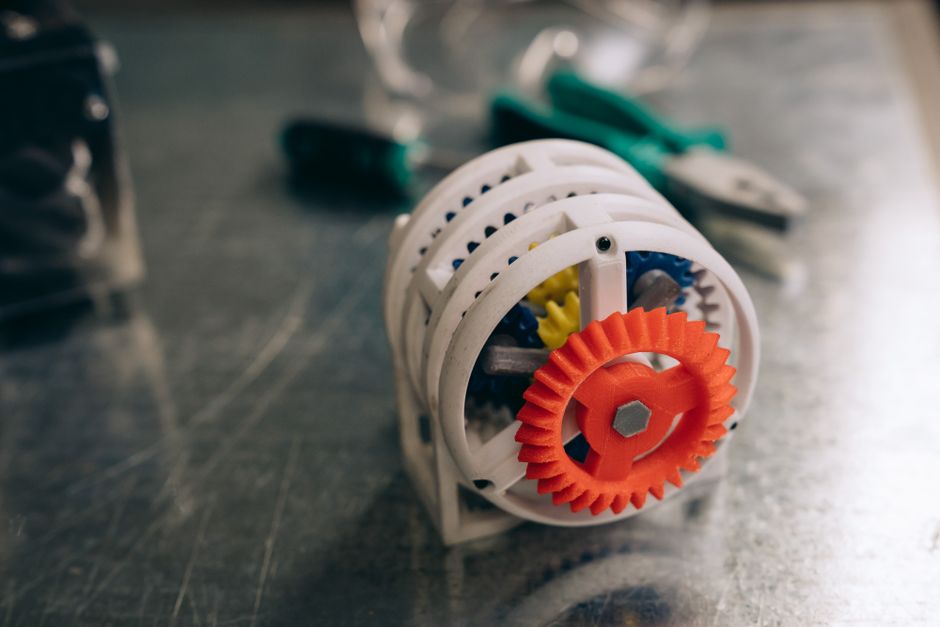
- Short- to mid-term performance: For many functional brackets, housings, and gears, PA6 can deliver excellent real-world durability when it’s properly dried and printed.
- Cost and availability (practically speaking): While prices change constantly, nylon 6 is commonly easier to source in the 3D printing filament ecosystem, which can help when you iterate.
What to watch
- Moisture sensitivity: Like most nylons, PA6 absorbs water. If it’s not dried and stored well, you can see stringing, rough surfaces, and weaker mechanical performance.
- Long-term creep can still matter: Under constant load and at elevated temperatures, nylon parts can slowly deform. If your design depends on strict shape retention for months or years, you may need a more careful material choice.
Nylon 12 for Low Creep and Higher Dimensional Stability
What it tends to do well
- Better shape retention under sustained load: PA12 is often the go-to when creep resistance is a design priority.
- Dimensional stability: If you’re making snap-fits, mounts, or mechanical components that must stay aligned, PA12 can be easier to manage after printing—again, assuming your drying and storage are solid.
- Performance in moisture-varying environments: While no nylon is “ignore moisture,” PA12 is often more forgiving in real-world humidity cycles.
What to watch
- Print workflow can be less forgiving: PA12 typically benefits from more disciplined printing conditions (dry filament, enclosure use, and stable bed adhesion).
- Toughness vs. stiffness tradeoffs: PA12 can still be tough, but “feel” and failure modes can differ from PA6. For highly dynamic parts, you may still want to prototype.
Nylon 6 vs Nylon 12: A Selection Framework
This is the practical way to decide which nylon fits your functional part—without guessing.
- Start with moisture control, not just “strength.” Nylon performance depends heavily on dryness at the moment you print. If you can reliably dry filament and keep it stored sealed with desiccant, either nylon can work well. If you can’t, choose the option that matches your realism: PA12 is often preferred when humidity exposure and consistency matter.
- Define the loading scenario and the time scale. Ask: is the part mostly loaded during assembly and occasional use, or is it under constant pressure/squeeze for weeks? For constant load and long-term fit, PA12 is usually the safer bet. For intermittent loads where toughness is the main goal, PA6 is often more practical.
- Account for temperature and enclosure limits. Both nylons like stable thermal conditions during printing. Enclosures help reduce warping and improve layer bonding. If your printer setup can’t maintain a warm, draft-free environment, you’ll likely fight quality on both materials—and that affects durability.
- Plan print settings around layer adhesion and dimensional control. Your goal is reliable bonding between layers, clean extrusion, and stable dimensions. In practice, that means: consistent nozzle/bed temperatures for nylon, slower speeds than you’d use for PLA, and a brim or other adhesion strategy when needed. PA12 may demand a bit more patience to hit the same “easy mode” feel.
- Think in terms of creep expectations, not max strength charts. Nylon creep is the gradual deformation that can occur under load. If your functional requirement is “keep clearance tight” or “maintain alignment,” you’re designing against creep. In those cases, PA12 tends to be the better starting point. If your requirement is “don’t crack under impact,” PA6 is often a strong choice.
- Prototype with the exact geometry that drives failure. The best nylon choice for a functional part is the one that survives your specific stress pattern. Print a small test with the thinnest critical section and the real load path (snap area, bearing pocket wall, rib). Let the prototype tell you whether creep, flex, or wear is the limiting factor.
- Treat drying and post-print conditioning as part of engineering. Dry filament before printing, then store it properly before the next print. After printing, allow parts to stabilize in a consistent environment. If your workflow includes post-processing (like annealing/heat conditioning), validate it with tests on the same nylon type—because dimensional results can differ.
Choose the Right Nylon Type for Common Functional Parts
Here’s a straightforward mapping from typical use cases to nylon choice.
- Snap-fit clips, brackets, and impact-prone parts: Often start with nylon 6 when toughness and robustness are the priorities. If the fit must stay tight under continuous pressure, move toward nylon 12.
- Bearings-adjacent components, low-friction housings, and wear surfaces: Both can work, but if the part must hold its shape during long-term loading, nylon 12 is commonly the safer direction.
- Threaded inserts and screw mounts: If creep would loosen alignment over time, nylon 12 is a strong starting point. For quick iterations and tough housings, nylon 6 is usually more forgiving to dial in.
- Parts that must maintain precision alignment: Go with nylon 12 when long-term dimensional stability matters more than “maximum toughness.”
- Parts used in dry-ish environments with disciplined printing: nylon 6 can be a great balance of durability and practicality.
The practical verdict: If your part is under constant load, needs to keep its dimensions, or lives through humidity swings, lean toward nylon 12. If the priority is tough, impact-resistant performance and you can keep moisture under control, nylon 6 is often the better first-material choice. The next step is simple: print a small functional test piece for your critical stress region using your real drying and enclosure setup, then choose based on how it holds up over time—not just in the first day after printing.
PriceIt3D may earn a commission when you buy through links on this page, at no extra cost to you. Affiliate notice.